

Table of Contents
In the highly demanding field of HVAC (Heating, Ventilation, and Air Conditioning) manufacturing, ensuring the long-term integrity and reliability of refrigeration circuits is paramount. A single, microscopic leak can lead to refrigerant loss, decreased energy efficiency, environmental hazards, and costly warranty claims. To prevent these issues, manufacturers rely on rigorous leak detection protocols. Among the most trusted methods is the Helium Leak Test System, renowned for its precision and reliability. Helium, an inert gas with extremely small and mobile molecules, can penetrate even the most minuscule leak paths, making it the ideal tracer gas.
However, within helium leak testing, manufacturers face a critical decision: should they employ a Vacuum Chamber method or a Sniffer method for their production lines? While both utilize helium to detect faults, their setup, sensitivity, and application differ significantly. This article provides a comprehensive comparison, ultimately highlighting why the Vacuum Chamber is the superior and most optimal choice for high-volume, high-precision HVAC Production.
Understanding the Methods: Sniffer vs. Vacuum Chamber
Before comparing their efficacy, it is essential to understand how each Helium Leak Test System operates.
The Sniffer Method
The Sniffer technique, also known as the accumulation or detector probe method, involves pressurizing the HVAC component (such as a coil or compressor) with helium or a helium-air mixture. An operator or a robotic arm then moves a handheld “sniffer” probe over the exterior surface, specifically targeting joints, brazed points, and seals. If a leak exists, the escaping helium is drawn into the probe and analyzed by a mass spectrometer.
The Vacuum Chamber Method
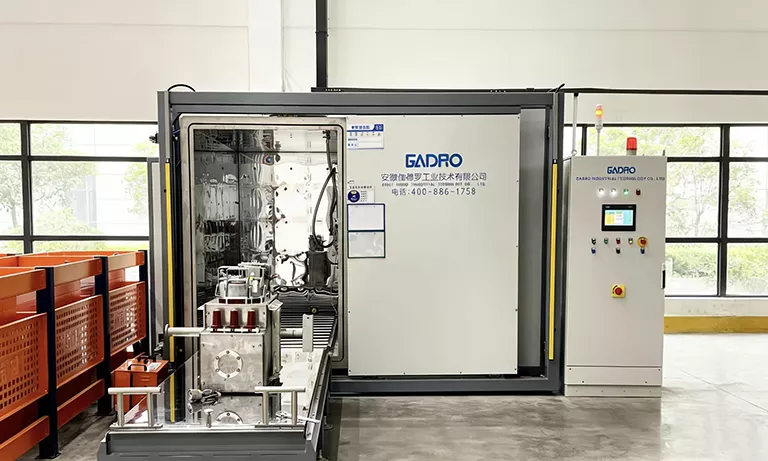
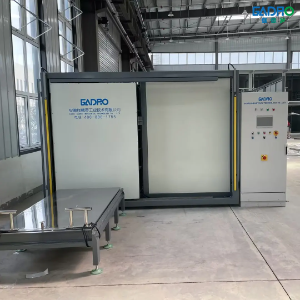
The Vacuum Chamber (or Hard Vacuum) method takes a more holistic and controlled approach. The entire HVAC component is placed inside a sealed Vacuum Chamber. A vacuum pump evacuates the air from both the chamber and the internal volume of the test part. Once a sufficient vacuum level is reached, the interior of the part is pressurized with helium. The mass spectrometer is connected to the Vacuum Chamber to continuously sample the space surrounding the part. If there is a leak, helium molecules will flow from the higher-pressure interior of the part into the evacuated chamber, where they are immediately detected.
Key Comparisons for HVAC Production
To determine which method is better suited for HVAC Production, we must evaluate them across several critical manufacturing criteria.
1. Sensitivity and Accuracy (The Vacuum Chamber Advantage)
The most significant difference between the two methods lies in their sensitivity ceilings.
- Sniffer Sensitivity: The Sniffer method is generally limited to detecting leak rates around 10⁻⁶ to 10⁻⁷ mbar·l/s. This limitation is primarily due to the natural background concentration of helium in the ambient air (approximately 5 ppm). When sniffing in an open factory environment, background noise can mask smaller leaks or lead to false positives.
- Vacuum Chamber Sensitivity: The Vacuum Chamber method excels in extreme sensitivity, capable of detecting leaks as minuscule as 10⁻⁹ to 10⁻¹² mbar·l/s. By operating in an evacuated environment, background helium is virtually eliminated. This allows the mass spectrometer to detect the faintest traces of helium escaping from the part, providing up to a million times more sensitivity than sniffing.
For modern HVAC Production, where environmental regulations regarding refrigerant emissions (like fluorinated greenhouse gases) are increasingly stringent, the ultra-high sensitivity of the Vacuum Chamber is not just an advantage; it is often a strict requirement.
2. Speed and Production Efficiency
In a high-volume manufacturing setting, cycle time is money.
- Sniffer Efficiency: Sniffing is inherently a localized test. It requires time to scan every individual joint and connection. If done manually, it is slow and highly dependent on the operator’s speed and technique. Even when automated with robotics, scanning complex geometries is time-consuming.
- Vacuum Chamber Efficiency: The Vacuum Chamber performs a global or integral test. It tests the entire component simultaneously. Once the chamber is evacuated and the part is pressurized, the mass spectrometer instantly detects any escaping helium, regardless of where the leak is located on the part. Automated in-line Vacuum Chamber systems can achieve extremely fast cycle times, easily handling high-production rates (e.g., testing over a hundred units per hour) with minimal downtime.
3. Reliability and Repeatability
- Sniffer Reliability: The Sniffer method is susceptible to human error. If an operator moves the probe too quickly, holds it too far from the surface, or misses a joint entirely, a leak can easily go undetected. Furthermore, fluctuations in factory air currents can blow leaking helium away from the probe.
- Vacuum Chamber Reliability: The Vacuum Chamber offers an objective, automated, and highly repeatable process. Because the test is conducted in a sealed, controlled vacuum environment, external factors like air drafts or operator technique are completely removed from the equation. The results are strictly quantifiable and verifiable, ensuring consistent product quality.
4. Qualitative vs. Quantitative Data
- Sniffer Data: Sniffing is primarily used for leak localization (finding where the leak is). While it provides a signal, quantifying the exact total leak rate of a component is difficult because the probe may only capture a fraction of the escaping gas.
- Vacuum Chamber Data: The Vacuum Chamber provides precise, quantitative data (measuring how much it is leaking globally). It measures the total leak rate of the entire assembly, allowing manufacturers to definitively pass or fail a product based on strict engineering specifications and industry standards.
Comparison Summary Table
| Feature | Vacuum Chamber Method | Sniffer Method |
| Test Type | Global / Integral (Tests whole part at once) | Localized (Scans specific areas) |
| Sensitivity | Ultra-High (up to 10⁻¹² mbar·l/s) | Moderate (up to 10⁻⁶ mbar·l/s) |
| Background Interference | None (Operates in a vacuum) | High (Susceptible to ambient helium) |
| Cycle Time | Very Fast (Automated, simultaneous testing) | Slower (Requires scanning entire surface) |
| Operator Dependency | Low (Fully automated process) | High (Manual scanning prone to human error) |
| Data Output | Quantitative (Exact total leak rate) | Qualitative/Semi-Quantitative (Best for locating) |
| Best Application | High-volume HVAC Production, critical compliance | Field service, large unwieldy assemblies, locating specific faults after a failed global test |
Why Vacuum Chamber is the Ultimate Choice for HVAC Production
When establishing a Helium Leak Test System for a modern HVAC manufacturing line, the Vacuum Chamber emerges as the unequivocal superior choice.
The primary goal of production-line testing is to ensure that no defective product leaves the factory. The Vacuum Chamber guarantees this by providing an infallible, highly sensitive, global test of the entire component. It removes the variability of human operators, eliminates the interference of ambient factory conditions, and provides concrete, measurable data that ensures compliance with stringent environmental and safety regulations.
While the Sniffer method has its place—specifically in field maintenance or for pinpointing the exact location of a leak after a component has failed a Vacuum Chamber test—it is generally insufficient as the primary quality control gate in high-volume manufacturing. The risk of missing a micro-leak due to background noise or operator error is simply too high.
Investing in a Hard Vacuum system represents a commitment to the highest quality standards. It ensures the longevity of the HVAC units, protects the environment from refrigerant leaks, and ultimately protects the manufacturer’s brand reputation from the costly consequences of field failures. For accuracy, speed, and absolute reliability, the Vacuum Chamber is the gold standard for HVAC leak detection.
FAQ
Can a component be damaged by the Vacuum Chamber test?
Generally, no, provided the component is designed to handle pressure differentials. The test is non-destructive. However, the component must be structurally capable of withstanding the external vacuum while being internally pressurized. For standard rigid HVAC components like compressors and metal coils, this is never an issue.
Is helium expensive, and does the Vacuum Chamber use a lot of it?
Helium can be a significant operational cost. However, modern automated vacuum test systems are almost always integrated with Helium Recovery Systems. These systems capture the helium after the test cycle, purify it, and reuse it for subsequent tests, recovering up to 95-98% of the gas and drastically reducing long-term operational costs.
If a part fails the Vacuum Chamber test, how do I find exactly where the leak is?
This is where a hybrid approach is often used. The Vacuum Chamber acts as the primary “Pass/Fail” gate. If a part fails the global vacuum test, it is removed from the automated line and taken to a rework station. There, an operator will use the Sniffer method to manually scan the pressurized part, pinpointing the exact location of the faulty weld or seal so it can be repaired.